Material Extrusion can look straightforward, but international purchasing rarely is. For global buyers, reliable sourcing begins long before a purchase order is issued. A profile may match a drawing yet fail during assembly, shipping, or outdoor use. Differences in resin grades, die design, cooling, and measurement methods can change performance. Small errors compound. This guide presents seven practical tips shaped by supplier reviews, sample checks, and production follow-up. It focuses on decisions that protect quality, cost control, and delivery reliability.
Start with a precise specification. State dimensions, tolerances, surface finish, color, resin, additives, and expected service conditions. Ask how the supplier measures each critical feature. Photos are not enough. A competent manufacturer should provide process details, inspection records, and clear material documentation. Request samples from regular production, not specially prepared pieces. They reveal warpage, color variation, surface marks, and fit problems early. Do not ignore packaging requirements. Moisture, dust, and heat can damage profiles before they reach your facility.
Cost deserves a wider lens. Tooling, testing, minimum order quantities, freight, duties, and rejected parts affect the final figure. Clear communication also matters. Time-zone gaps and vague revision control often create avoidable mistakes. Use written approvals, controlled drawings, and agreed inspection points. A supplier may be experienced yet unsuitable for your application. That uncertainty should be recorded, not hidden. The strongest buying decision balances capability, evidence, traceability, and realistic delivery commitments. Perfect plans rarely survive production. Good buyers leave room for review.
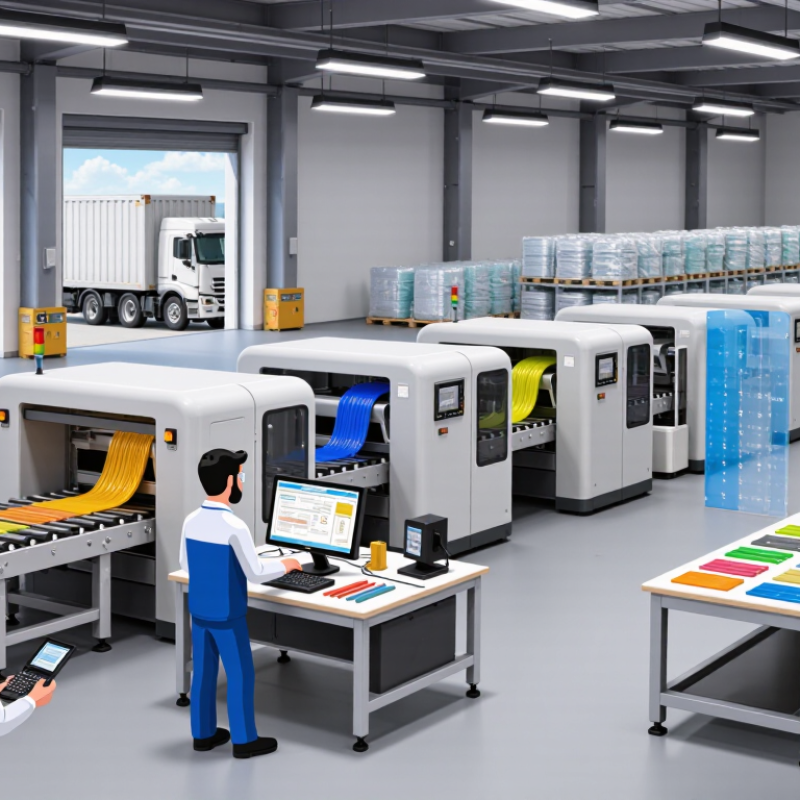
Material Extrusion Tips for Global Buyers: Know the Fundamentals
Material extrusion, or MEX, is defined in ISO/ASTM 52900 as a process that selectively dispenses material through a nozzle or orifice. The material is deposited layer by layer and fused, cooled, or otherwise solidified. Common feedstocks include thermoplastic filament, pellets, and specialized pastes. Buyers should confirm the exact process scope, because “extrusion printing” may describe different machines, materials, and production limits.
The terminology matters during international sourcing. Ask whether the supplier reports nozzle diameter, layer height, extrusion temperature, build volume, and dimensional tolerance using consistent methods. A 0.4 mm nozzle does not guarantee a 0.1 mm functional feature. Geometry, cooling, shrinkage, and toolpath direction still affect results. The Wohlers Report 2024 estimated the global additive manufacturing industry reached approximately 20.0 billion US dollars in 2023, with year-on-year growth of 13.5%. That growth increases supplier choice, but it can also increase specification confusion.
Look beyond impressive sample parts. Request test coupons, material certificates, and repeatability data from several build cycles. ISO/ASTM 52900 standardizes vocabulary, not machine quality or final-part performance. That distinction is easy to miss. In practice, buyers sometimes compare incompatible claims because “accuracy” lacks a shared measurement condition. A better purchase file defines material grade, moisture control, orientation, infill, post-processing, inspection method, and acceptance limits. Some details may feel excessive. They prevent expensive assumptions later.
| No. | Buyer Tip | ISO/ASTM 52900 Term or Concept | What the Term Means | Process Scope and Technical Relevance | Indicative Technical Data | Global Purchasing Checkpoint |
|---|---|---|---|---|---|---|
| 1 | Confirm that the technology is actually material extrusion. | Material extrusion (MEX) | An additive manufacturing process in which material is selectively dispensed through a nozzle or orifice. | The category includes systems that deposit thermoplastic, composite, ceramic-loaded, or metal-loaded feedstock in successive locations and layers. It is different from vat photopolymerization, powder bed fusion, and material jetting. |
Typical output: deposited roads or beads Common feedstock: filament, pellets, or specialized compound Primary control: material flow and toolpath |
Ask the supplier to state the process category, feedstock form, deposition method, and applicable standard terminology rather than relying only on informal process names. |
| 2 | Specify feedstock form and material condition. | Feedstock; material deposition | Feedstock is the material supplied to the process. Deposition describes how the material is placed through the nozzle or orifice. | Filament-fed equipment normally requires controlled diameter and low moisture. Pellet-fed equipment can support higher throughput and larger parts, but it may require more process development and material drying control. |
Common filament diameters: approximately 1.75 mm or 2.85 mm Typical layer height: about 0.05–0.40 mm, depending on nozzle and application Key variables: moisture, diameter tolerance, melt flow, contamination |
Include feedstock specification, moisture limit, storage conditions, dimensional tolerance, batch traceability, and whether recycled or filled material is permitted. |
| 3 | Compare build volume with the usable production envelope. | Build platform; build volume; build direction | The build platform supports the part during fabrication. Build volume is the usable three-dimensional region available for part production, while build direction identifies the orientation of deposition. | The nominal machine envelope may be larger than the practical envelope because of edge limitations, purge areas, clamps, thermal gradients, or required clearance around the part. |
Relevant axes: X, Y, and Z Usable volume factors: nozzle clearance, platform flatness, chamber temperature, support space Resolution trade-off: smaller layers generally increase build time |
Request the effective printable area, maximum continuous part size, permitted overhang, recommended orientation, and dimensional accuracy data measured on comparable geometries. |
| 4 | Match the thermal system to the polymer and part geometry. | Material extrusion process parameters | Process parameters are the controllable settings that influence deposition, bonding, geometry, and surface quality, including temperature, speed, layer height, and material flow. | Nozzle temperature, build-platform temperature, ambient temperature, and chamber temperature affect melt flow, cooling, warpage, and interlayer bonding. The correct settings depend on the material grade and equipment design. |
Illustrative nozzle-temperature ranges: PLA: about 180–230 °C ABS: about 230–260 °C Nylon/polyamide: about 240–280 °C PEEK: about 360–450 °C Actual values must follow the material supplier’s qualified process window. |
Verify heated-platform capability, chamber control, temperature uniformity, drying equipment, calibration procedure, and whether the supplier has validated the requested material on the proposed machine. |
| 5 | Evaluate supports, orientation, and anisotropy before approving the design. | Support structure; build orientation; anisotropy | Support structures hold overhangs or bridges during fabrication. Build orientation is the position of the part relative to the deposition axes. Anisotropy means that properties can vary with direction. | Material extrusion parts commonly show different strength, elongation, surface finish, and dimensional behavior between the deposition-plane directions and the layer-to-layer direction. Orientation also affects supports, stair-stepping, and post-processing. |
Typical design considerations: overhang angle, bridge length, wall thickness, infill percentage, raster direction, number of perimeter roads General effect: interlayer strength is often lower than in-plane strength |
Require orientation drawings, support-removal assumptions, critical-direction mechanical data, surface-finish expectations, and acceptance samples using the final material and process settings. |
| 6 | Separate terminology compliance from part-quality compliance. | ISO/ASTM 52900 vocabulary and process classification | ISO/ASTM 52900 establishes general additive-manufacturing principles and vocabulary. It does not, by itself, certify a machine, approve a material, or guarantee the performance of a finished part. | A supplier can correctly identify a process as material extrusion while still needing separate controls for dimensional inspection, mechanical testing, surface quality, traceability, and production acceptance. | Quality records may include: machine identification, material batch, drying history, parameter file, build orientation, environmental conditions, inspection results, and nonconformance records | Put measurable requirements in the purchase specification: tolerances, test method, sampling plan, appearance limits, material certification, process records, and change-control obligations. |
| 7 | Calculate total landed cost and compliance risk, not only machine or part price. | Post-processing; finished part; process chain | The process chain includes preparation, material conditioning, deposition, cooling, support removal, machining or surface treatment, inspection, packaging, and delivery. | Material extrusion economics depend on material consumption, build time, support waste, labor, drying, failed builds, post-processing, energy, maintenance, tooling, and cross-border logistics. A lower quoted unit price may not represent a lower total cost. |
Total-cost elements: feedstock + machine time + labor + supports/waste + post-processing + inspection + packaging + freight + duties/taxes Useful KPI: accepted parts per build and cost per accepted part |
Request a landed-cost model, annual maintenance assumptions, spare-part lead times, electrical and safety documentation, export/import information, and a clear definition of what is included in the quoted price. |
| Reference note: Terminology and process classification are based on ISO/ASTM 52900:2021, Additive manufacturing — General principles — Fundamentals and vocabulary. Temperature ranges, layer heights, and dimensional examples are indicative engineering ranges rather than requirements of the standard; final values must be validated for the selected equipment, material grade, geometry, and acceptance criteria. | ||||||
Material extrusion deposits material through a nozzle or opening. It builds parts layer by layer. The material may cool, fuse, or solidify.
Common feedstocks include thermoplastic filament, pellets, and specialized pastes. Confirm the exact material grade before purchasing. Different feedstocks require different temperatures and handling.
No. Nozzle size does not guarantee functional feature accuracy. Cooling, shrinkage, geometry, and toolpath direction also matter.
Layer heights between 0.1 and 0.3 mm often balance surface finish and production speed. Smaller layers can increase printing time. They may also expose warping or alignment problems.
Request nozzle diameter, layer height, extrusion temperature, build volume, and tolerance data. Ask for results from several build cycles. One attractive sample proves very little.
Request test coupons and measurements across several axes. A 100 mm gauge block can reveal scaling errors. A hole and thin wall reveal different weaknesses. Measure repeatedly.
An initial tolerance around ±0.2–0.3 mm may be realistic for many parts. Material shrinkage, geometry, and calibration can change the result. Do not promise ±0.1 mm too quickly.
Define material grade, moisture control, orientation, infill, post-processing, and inspection methods. Include acceptance limits and repeatability requirements. Some details feel excessive. They prevent expensive assumptions later.
Confirm the delivery term, named location, customs responsibilities, and risk transfer. Check tariff classification before ordering. Request invoices, packing lists, and origin documents. One overlooked port charge may erase the expected saving.
Include product cost, tooling, packaging, transport, insurance, duties, taxes, testing, storage, and possible scrap. Add a contingency allowance. Estimates can still be wrong. A pilot shipment and incoming inspection provide stronger control.
Material Extrusion is a practical manufacturing method, but global buyers should evaluate it through clear technical and commercial standards. Begin by understanding ISO/ASTM 52900 terminology, process scope, and the differences between equipment, feedstock, and finished parts. Define quality targets before requesting quotations, including layer heights of approximately 0.1–0.3 mm, suitable 0.4 mm nozzles, dimensional tolerances, surface expectations, and inspection methods. Material selection should rely on measurable data such as glass transition temperature, moisture limits, drying requirements, and verified ASTM or ISO test results.
Supplier evaluation should include ISO 9001 practices, batch traceability, production capacity, quality records, and realistic lead times. Buyers should also calculate total landed cost rather than focusing only on unit price. This includes Incoterms, duties, shipping, packaging, applicable CE or REACH requirements, warranty terms, technical support, and potential rework costs. A structured comparison of these factors can reduce quality variation, delivery surprises, and import-related risks while supporting reliable long-term sourcing.
 XinYe Metal