2026 Top Extrusion Industry Types for Global Buyers

Time:2026-10-16 Author:Liam
0%

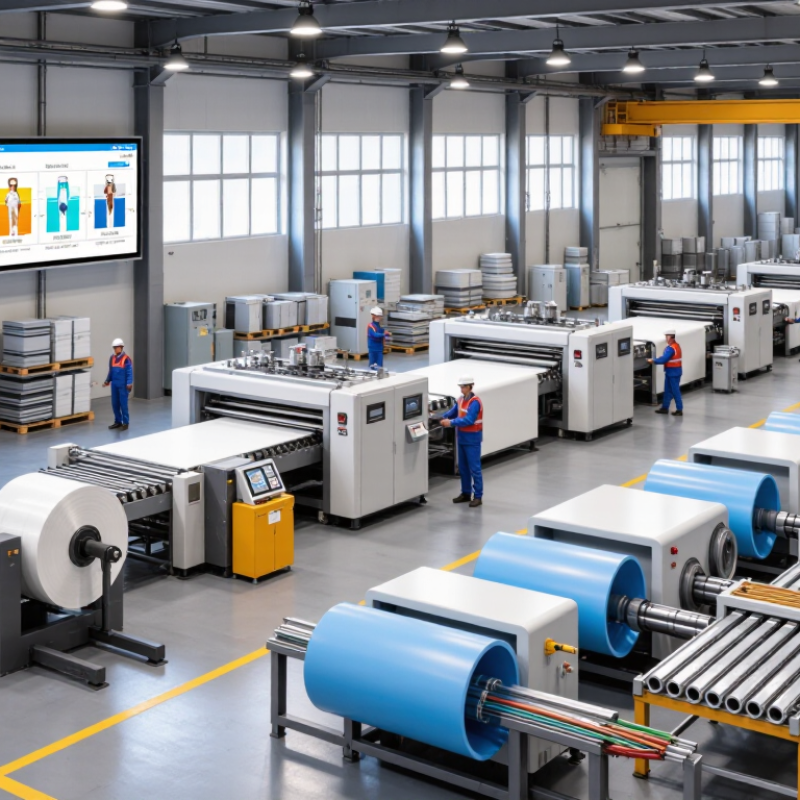
Global buyers enter 2026 with a wider choice of extrusion technologies than ever. The Extrusion Industry now covers film, sheet, pipe, profile, cable coating, and aluminum systems. Each type serves a different production reality. A food-packaging line may prioritize barrier film and high-speed cooling. A construction buyer may need rigid profiles, stable dimensions, and long-term weather resistance.

The OECD’s Global Plastics Outlook reports that worldwide plastics production reached 460 million tonnes in 2019. That volume shows the scale behind extrusion demand. Smithers’ packaging forecasts also identify flexible packaging, recyclable structures, and downgauging as important market directions through the decade. Meanwhile, International Aluminium Institute data continues to show aluminum’s growing role in transport, construction, and lightweight engineering. These reports provide useful context, but forecasts can still miss regional disruptions, energy-price changes, or sudden material shifts.

Quality remains more than a catalog specification. Die design, melt temperature, cooling speed, screw configuration, and operator experience can change the final result. Extrusion expert Chris Rauwendaal writes, “The goal of extrusion is to produce a product with the desired shape, dimensions, and properties at the lowest possible cost.” That principle remains practical in 2026. The cheapest machine is rarely the cheapest solution. A poorly matched line can create visible weld lines, uneven thickness, excess scrap, and costly downtime. This guide compares the leading extrusion industry types for global buyers, while recognizing one limitation: no universal ranking fits every plant, polymer, climate, or end-use requirement.
2026 Top Extrusion Industry Types for Global Buyers

Extrusion Industry Taxonomy: Metal, Polymer, Rubber, and Ceramic Routes

For global buyers, extrusion begins with route selection, not machine capacity. Metal extrusion shapes aluminum, copper, and steel into profiles, tubes, and structural sections. It demands controlled billets, high forming pressure, accurate die design, and careful heat treatment. A bright surface can still hide internal cracks. That detail matters. Buyers should request tensile data, dimensional tolerances, and traceable inspection records.

Polymer extrusion handles thermoplastics through heated barrels and calibrated dies. It produces film, pipe, insulation, sheets, and complex profiles at high volume. Resin moisture, melt temperature, cooling speed, and die swell directly affect consistency. Rubber extrusion uses compounds that need different curing behavior and dimensional control. Seals, hoses, and weather strips may look simple, yet surface defects can signal poor mixing or uneven vulcanization. Buyers should compare compound formulation, hardness, compression set, and aging performance. That shortcut often fails.

Ceramic extrusion serves applications requiring heat resistance, electrical insulation, or chemical stability. A plasticized ceramic mass passes through a die, then undergoes drying and firing. Shrinkage during firing is the difficult variable. Small moisture differences can distort long channels or create hidden fractures. Reliable evaluation includes density, porosity, thermal shock results, and fired dimensions. Cross-route comparisons can mislead; a polymer tolerance cannot be transferred to a fired ceramic part. Even a strong specification may need revision after pilot production. That is where practical judgment matters.

Aluminum Extrusion: 6xxx Alloys, ASTM B221, and Profile Applications

Aluminum extrusion remains a practical choice for global buyers seeking strong, lightweight profiles. The 6xxx series, including 6061 and 6063, offers useful combinations of strength, corrosion resistance, and machinability. Alloy selection should follow the application, not habit. Fit matters more.

ASTM B221 defines requirements for extruded aluminum bars, profiles, tubes, and related products. It can support consistent purchasing across international supply chains. However, citing ASTM B221 alone is not enough. Buyers should confirm the alloy, temper, dimensions, tolerances, surface condition, and mechanical test requirements. A certificate should connect these details to the production lot.

6063 is commonly selected for architectural frames, railings, lighting channels, and clean-looking enclosures. Its surface quality often suits anodizing and visible applications. 6061 generally serves heavier structural components, machine frames, transport parts, and load-bearing assemblies.

Actual performance depends on temper, wall thickness, geometry, and joining methods. Small details matter. A profile may look excellent and still distort during welding or machining.

In sourcing reviews, dimensional inspection and straightness checks often reveal issues missed by visual approval. Some buyers also overlook packaging, causing scratches before the material reaches fabrication. That assumption fails.

Request clear drawings, inspection records, alloy certificates, and traceability before approving volume production. When requirements remain vague, even a technically compliant extrusion may not fit the finished product.

Plastic Extrusion: PE, PP, and PVC with 150–250°C Melt Ranges

2026 Top Extrusion Industry Types for Global Buyers

Plastic extrusion buyers often compare PE, PP, and PVC by melt temperature. The practical range usually sits between 150°C and 250°C. Actual settings depend on grade, additives, screw design, and product thickness.

PE

PE commonly melts around 150–210°C. It suits films, pipes, sheets, and flexible profiles. Operators should watch die pressure and cooling speed. Uneven cooling can create shrinkage, waviness, or weak edges.

PP

PP generally requires about 180–240°C. It offers useful stiffness and chemical resistance. A stable feed zone helps prevent surging. I have seen excessive heat produce a glossy surface but lower impact strength. That result looked acceptable at first.

PVC

PVC often processes near 160–200°C, although formulations vary widely. It needs careful temperature control because extended residence time may cause discoloration or degradation. Venting also matters, especially with rigid profiles. A sharp odor or brown streak deserves immediate investigation.

Global buyers should request melt-temperature records, output testing, and sample dimensions. Do not rely only on a machine’s maximum temperature. Barrel readings can differ from the polymer’s real melt condition. A thermal camera, pressure chart, and simple cut-section inspection reveal more.

My field notes are not perfect. Material suppliers sometimes publish broad ranges, while production lines behave differently. Trial runs should record torque, pressure, cooling-water temperature, and surface quality. Small changes in screw speed can alter the entire extrusion window.

Hot, Cold, and Impact Extrusion: Force, Tolerance, and Output Metrics

2026 Top Extrusion Industry Types for Global Buyers

Hot, cold, and impact extrusion differ mainly in force, tolerance, and output. Hot extrusion commonly heats aluminum billets near 400–500°C. This reduces flow resistance and supports larger profiles at steady production rates. Cold extrusion works near room temperature. It demands higher press force, but often delivers cleaner surfaces and tighter dimensions. Impact extrusion uses a rapid stroke to form cups, shells, and short hollow parts. Its force peak arrives quickly. Real production lines rarely behave so neatly.

The International Aluminium Institute reported approximately 72 million tonnes of global primary aluminum production in 2024. That scale increases pressure for efficient downstream forming. The U.S. Department of Energy’s Industrial Decarbonization Roadmap also identifies metal forming as an important energy-performance area. Buyers should compare tonnes per hour, ram pressure, billet temperature, die life, scrap rate, and dimensional capability. EN 755-9 and ISO 286-2 can support tolerance discussions, but they do not replace process trials. A catalogue tolerance may fail after heat treatment or long-distance shipping.

Tips: Ask suppliers for force curves, not only maximum press tonnage. Request Cpk data from recent batches. Check wall thickness at the thinnest corner. Also measure exit temperature and surface defects. One practical warning: higher output may increase die wear and correction work. The cheapest cycle can become the least reliable one.

2026 Buyer Criteria: Die Design, ISO 9001, Capacity, and Total Cost

In 2026, global buyers will compare extrusion types by application, not machinery alone. Film, pipe, profile, sheet, and wire extrusion serve different risk profiles. PlasticsEurope reported 413.8 million tonnes of global plastics production in 2023. That volume signals sustained demand, but it does not guarantee profitable output.

Die design should match resin behavior, wall tolerance, and expected changeovers. Ask for flow simulations, die steel specifications, polishing standards, and sample measurements. A narrow tolerance can reduce scrap, yet an overly complex die may increase maintenance costs. Check actual trial data, not only catalog claims. Small details matter.

ISO 9001 certification remains a useful process-control signal. The ISO Survey recorded more than one million valid ISO 9001 certificates worldwide, showing its broad industrial adoption. Certification is not proof of perfect production. Review corrective-action records, calibration intervals, traceability, and incoming-material controls. Capacity deserves equal scrutiny. Compare rated output with sustained output under your resin, profile, and cooling conditions. The gap can be uncomfortable.

Total cost should include tooling, energy, labor, maintenance, rejected material, logistics, and downtime. The lowest quotation may become expensive after several die adjustments. A practical buyer can request a 72-hour production trial, verified kilogram-per-hour results, and dimensional reports from three batches. This is not always convenient. It is often more reliable than a polished presentation. Reports from market analysts can guide forecasts, but site evidence should decide the purchase.

FAQS

What is the main difference between hot, cold, and impact extrusion?

Hot extrusion heats billets near 400–500°C, reducing flow resistance. Cold extrusion works near room temperature and needs higher force. Impact extrusion uses a rapid stroke for cups, shells, and short hollow parts. Real lines behave less neatly.

When is hot extrusion a suitable choice?

Hot extrusion suits larger profiles and steady output. Heated aluminum flows more easily. However, heat can affect dimensions, surfaces, and energy costs. Trial data matters.

What advantages does cold extrusion provide?

Cold extrusion often produces cleaner surfaces and tighter dimensions. It demands stronger presses and higher force. Inspect cracking, tool wear, and actual wall thickness.

What should buyers compare besides maximum press tonnage?

Request force curves, not only peak tonnage. Compare sustained output, billet temperature, die life, scrap rate, and tolerance capability. Maximum force can hide unstable production.

How can buyers verify a supplier’s real capacity?

Ask for a 72-hour production trial. Measure kilograms per hour under your material and cooling conditions. Compare rated output with sustained output. The gap is uncomfortable.

What details should buyers inspect in die design?

Check flow simulations, die steel, polishing quality, and changeover time. Match the die with material behavior and wall tolerance. A complex die may reduce scrap but increase maintenance.

Does quality certification guarantee reliable extrusion?

No. Certification suggests process control, not perfect production. Review calibration records, material traceability, corrective actions, and incoming-material checks. Documents can still miss practical defects.

What should total cost include when comparing quotations?

Include tooling, energy, labor, maintenance, rejected material, logistics, and downtime. A low quotation may require repeated die adjustments. I would not trust price alone.

Which production measurements deserve close attention?

Check kilograms per hour, exit temperature, surface defects, and the thinnest wall corner. Request dimensional reports from three batches. Higher output can increase die wear and correction work.

Conclusion

The 2026 Extrusion Industry is defined by diverse processing routes for metal, polymer, rubber, and ceramic materials, each serving distinct performance and application needs. Aluminum extrusion remains especially important, with 6xxx-series alloys commonly selected for their balance of strength, formability, corrosion resistance, and recyclability. Buyers should also consider ASTM B221 requirements when evaluating structural profiles, frames, transport components, heat-transfer parts, and other engineered applications.

Plastic extrusion continues to rely heavily on PE, PP, and PVC, with typical melt-processing ranges of approximately 150–250°C depending on material grade and formulation. Hot, cold, and impact extrusion offer different combinations of forming force, dimensional tolerance, surface quality, and production output. For 2026 sourcing decisions, buyers should assess die design, process stability, ISO 9001 quality systems, production capacity, maintenance capability, delivery reliability, and total cost. A complete evaluation should balance material efficiency, tooling investment, energy use, quality consistency, and long-term operational value rather than focusing only on the initial purchase price.
Liam

Liam

Liam is a dedicated marketing professional with a profound expertise in the industry, where he excels at highlighting the unique advantages of our core products. With a keen understanding of market trends and consumer needs, Liam frequently updates our company’s professional blog, providing......